Assembly & Process Automation

Assembly around the process

Assembly & Process Automation

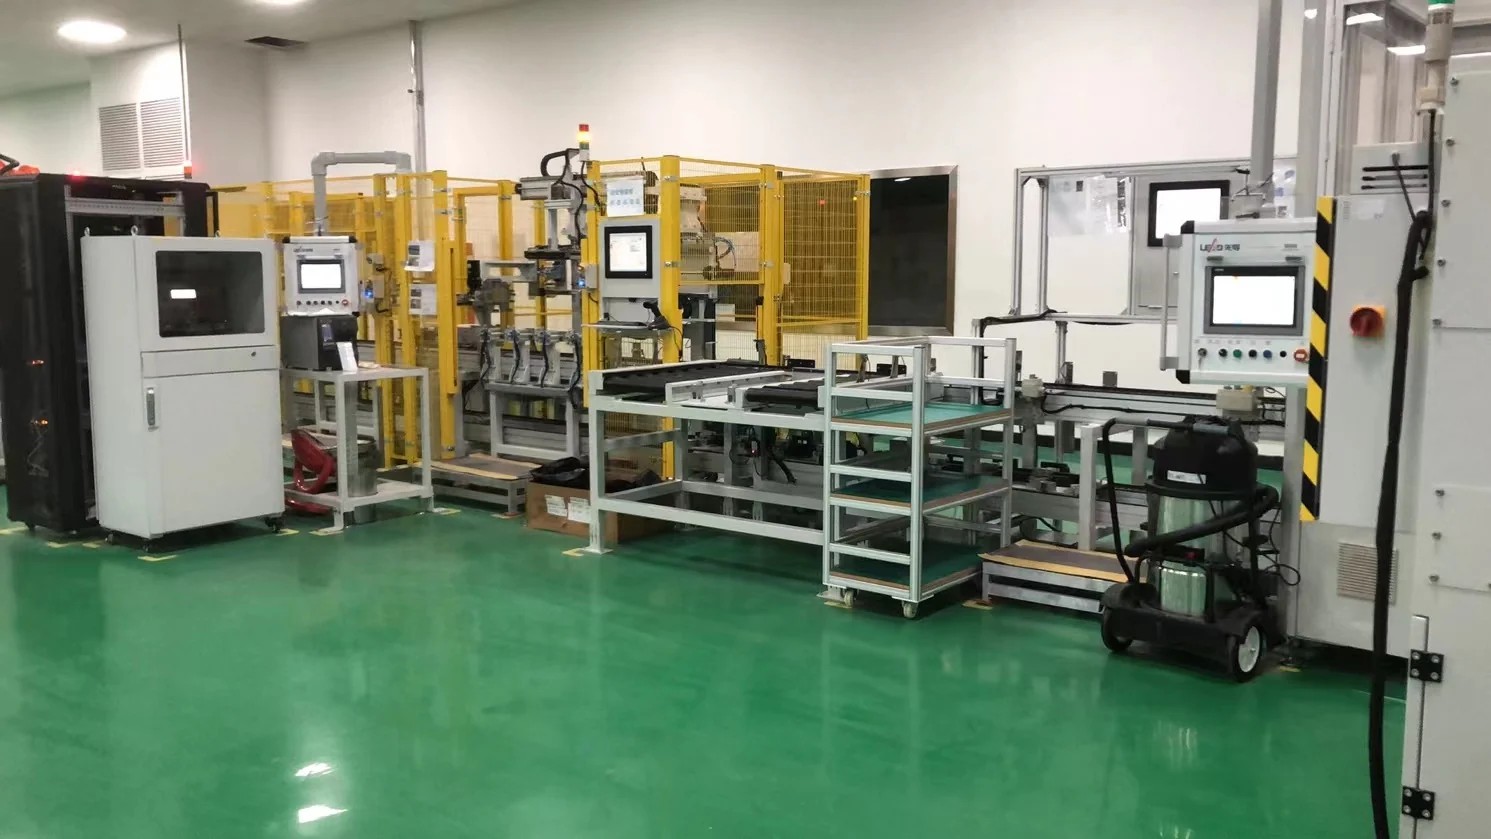
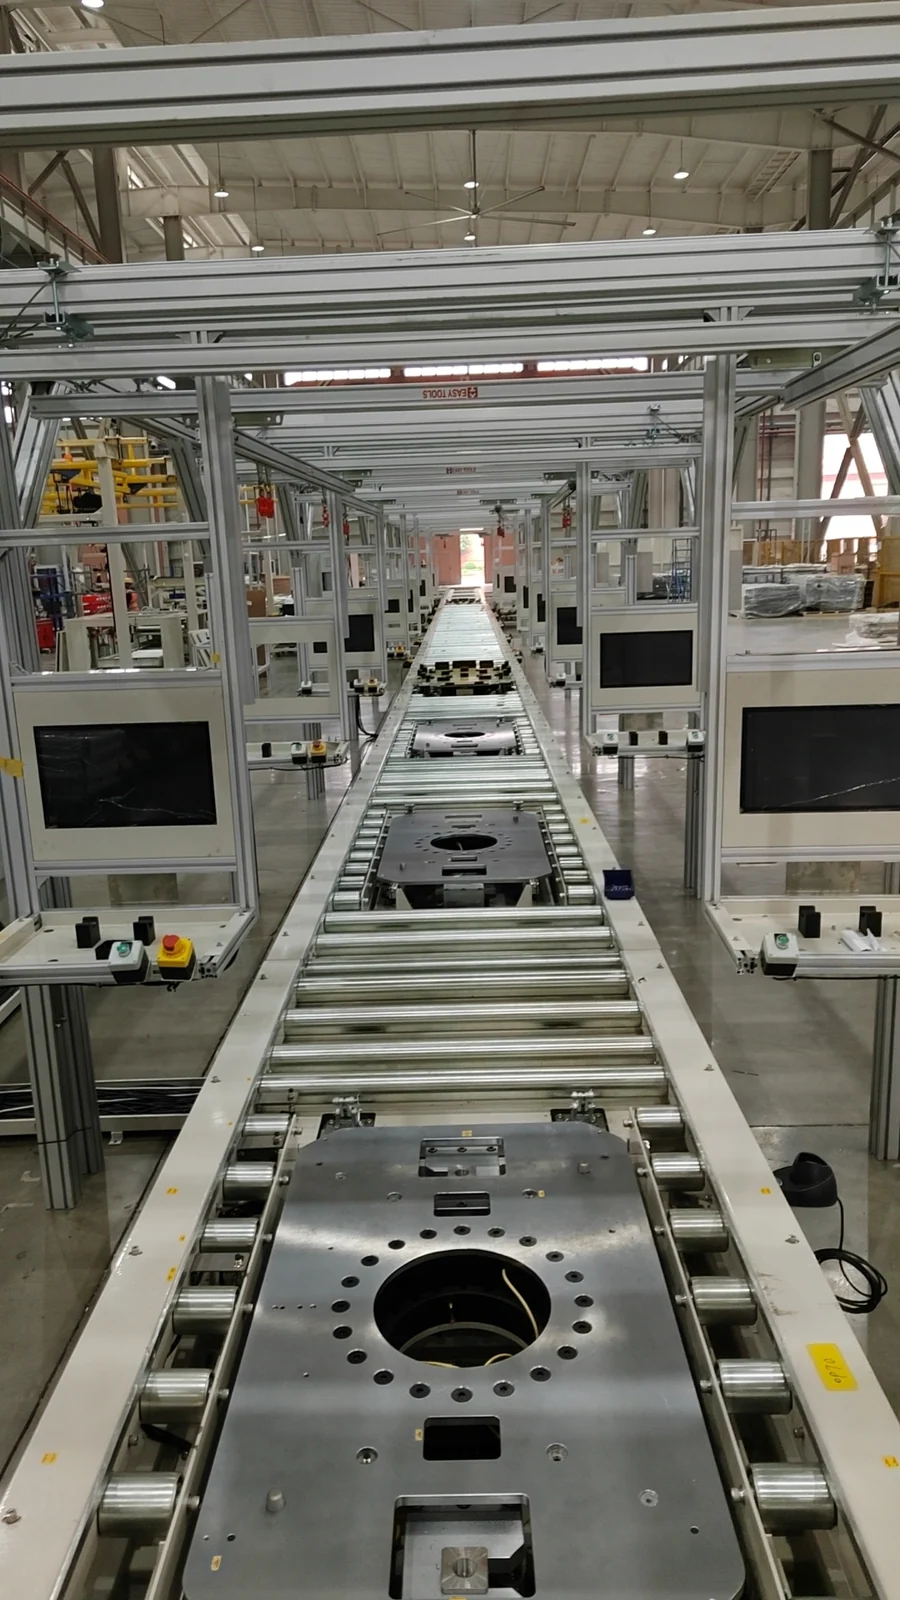
We integrate assembly stations, dedicated mechanisms and automated processes around the product, cycle time and actual production requirements.

  • Process integration
  • Station coordination
  • Process confirmation
  • Equipment interlocks

Assembly Systems

Automated & Semi-Automated Assembly Stations

Automated & Semi-Automated Assembly Stations

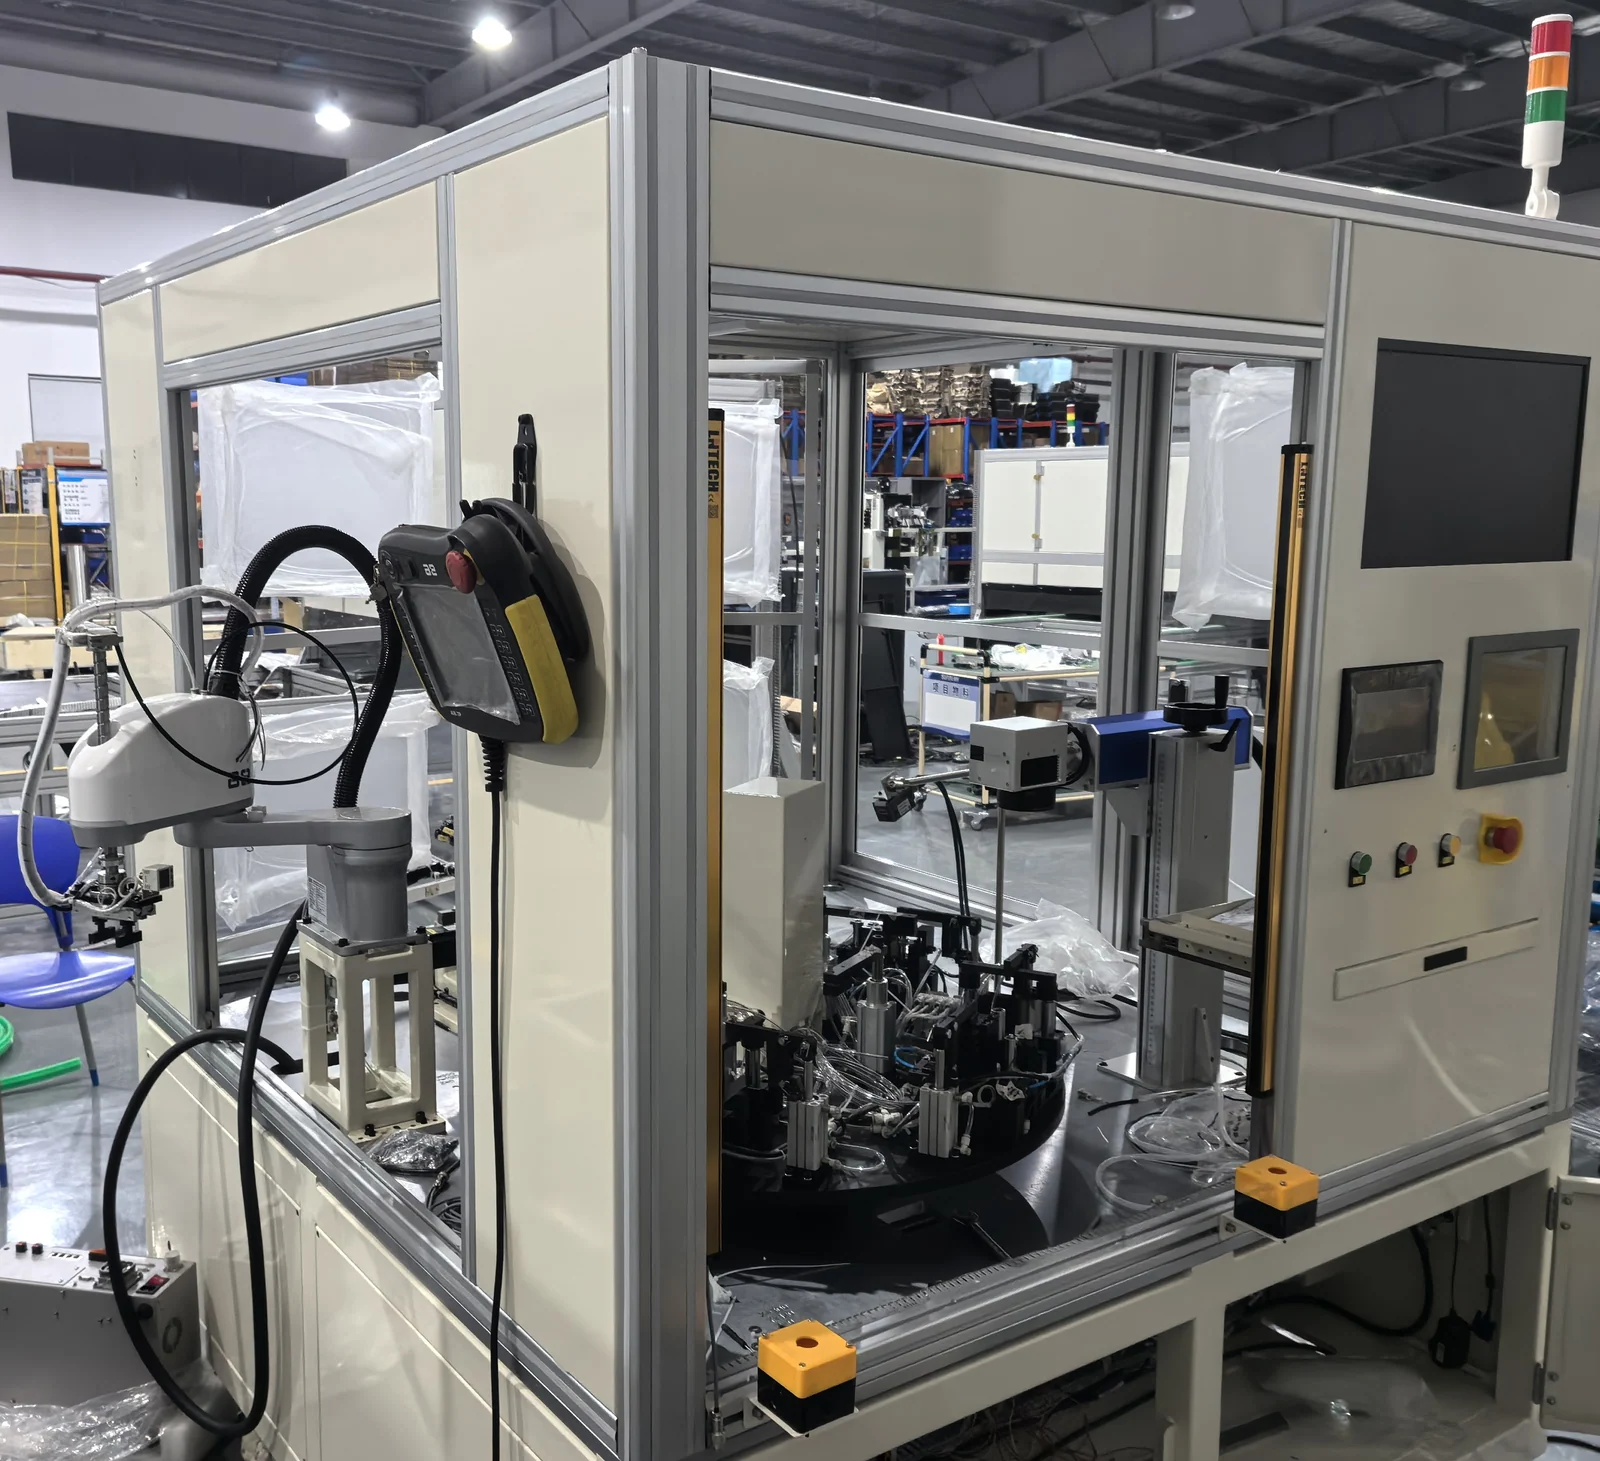
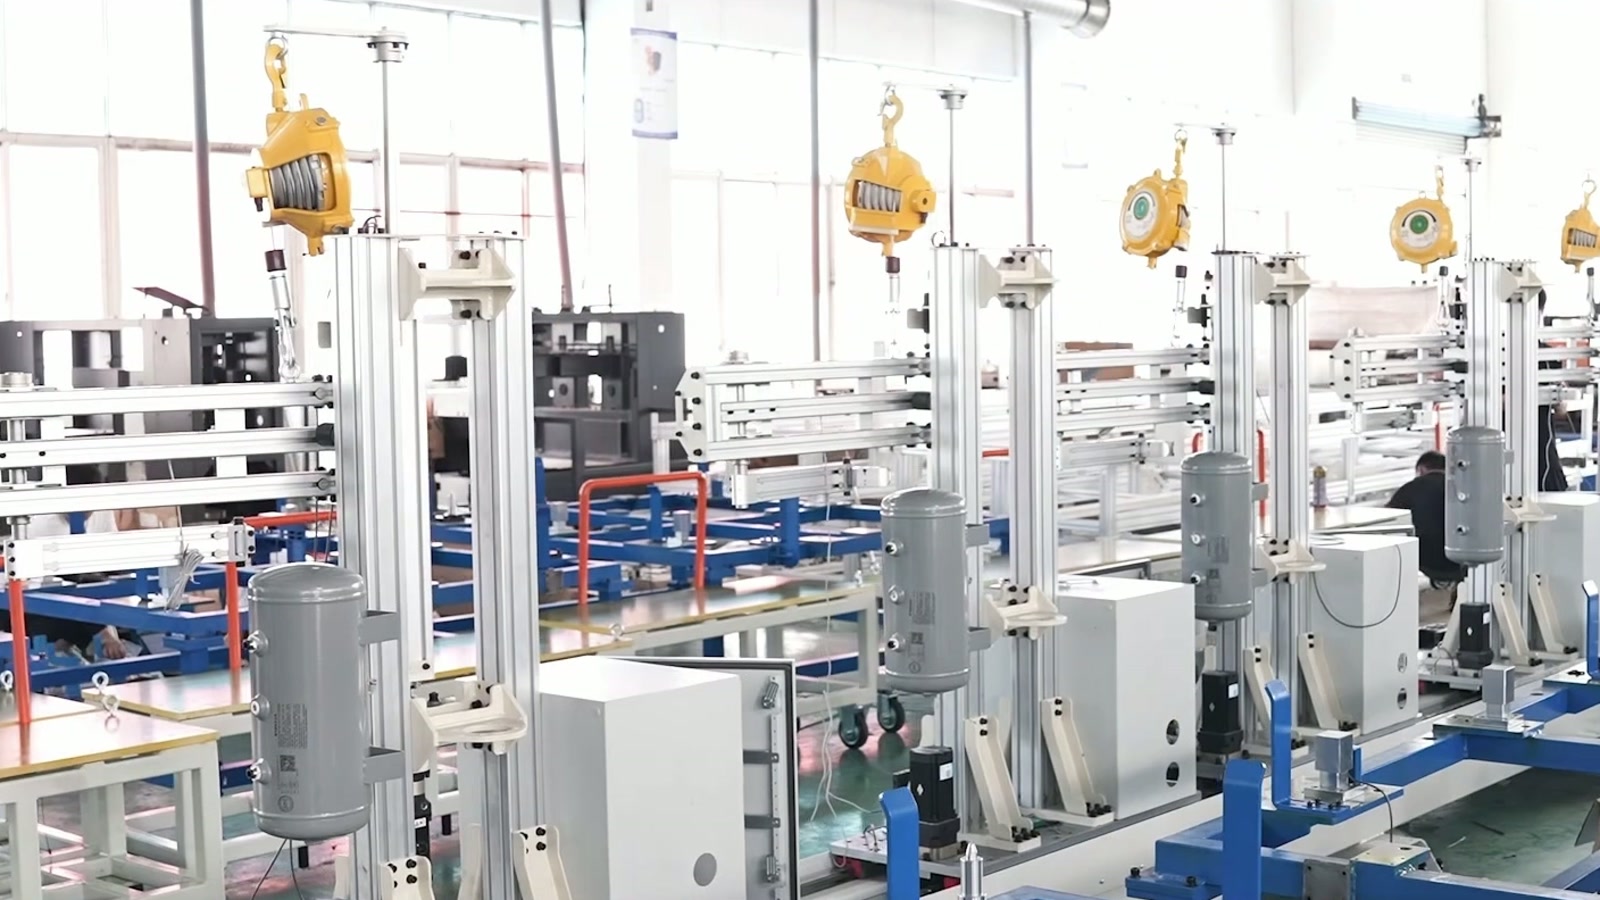
Manual work, dedicated mechanisms, sensors, fixtures and controls are combined according to the assembly process. A station can support assisted assembly, automatic operations, error-proofing, process confirmation and result feedback.

  • Assisted assembly
  • Workholding fixtures
  • Process confirmation
Multi-Station Assembly Systems

Multi-Station Assembly Systems

Multiple stations are organized around the assembly sequence, cycle time and equipment interfaces. Workpiece movement and operating logic are coordinated between stations.

  • Operation sequence
  • Cycle coordination
  • Workpiece transfer
Assembly Line Integration

Assembly Line Integration

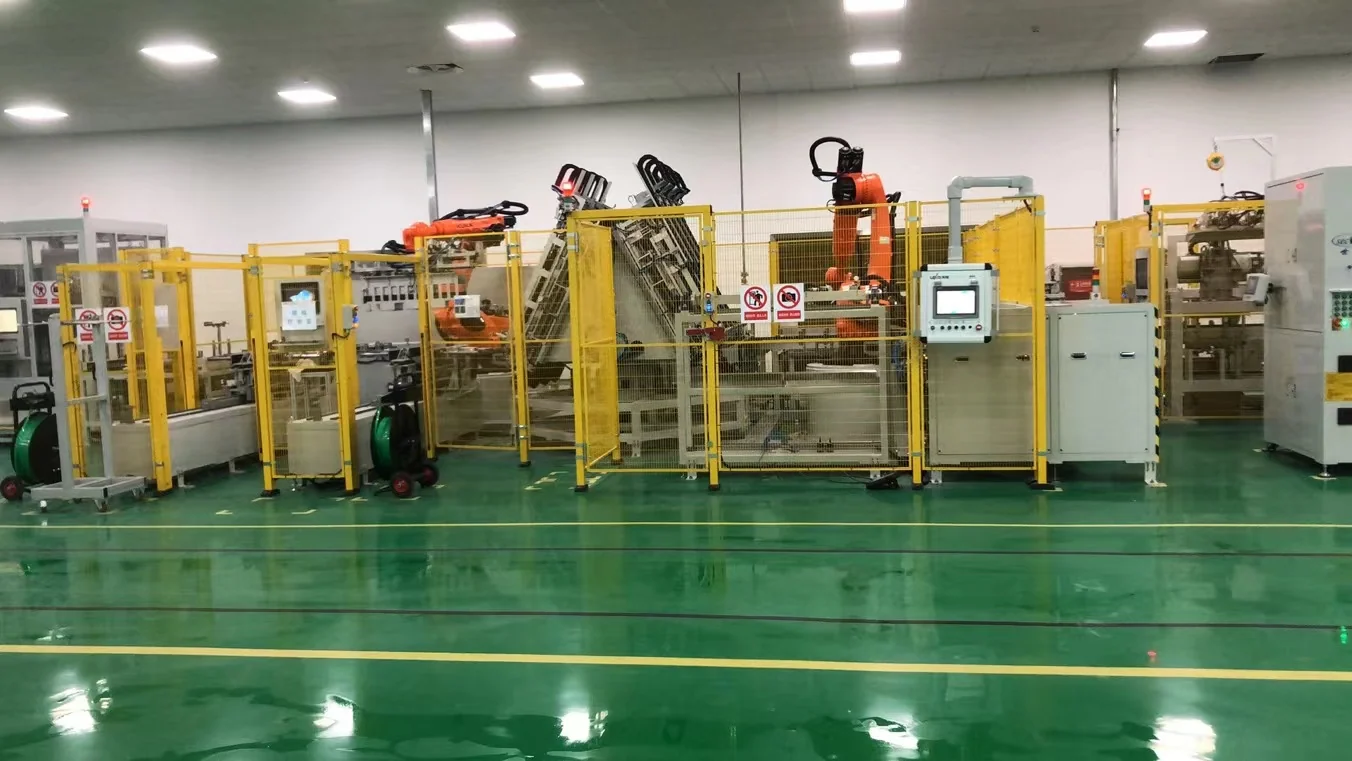
Assembly stations, conveyors, robots, inspection and testing are connected into a complete production flow. Equipment interfaces, cycle-time relationships and control coordination are considered together rather than as separate machines.

  • Equipment interfaces
  • Control coordination
  • Inspection interfaces
Coordination Between Manual & Automated Stations

Coordination Between Manual & Automated Stations

Manual operations are retained where appropriate and connected with automated stations through positioning, error-proofing, release logic and interlocks. Full automation is not the only objective.

  • Manual operations
  • Error-proof positioning
  • Release interlocks

Process Modules

Press-fitting

Pressing actions, position and process control are defined by the actual application. Fixtures, sensors and controls are integrated around these requirements.

Riveting & Rivet Pressing

Riveting & Rivet Pressing

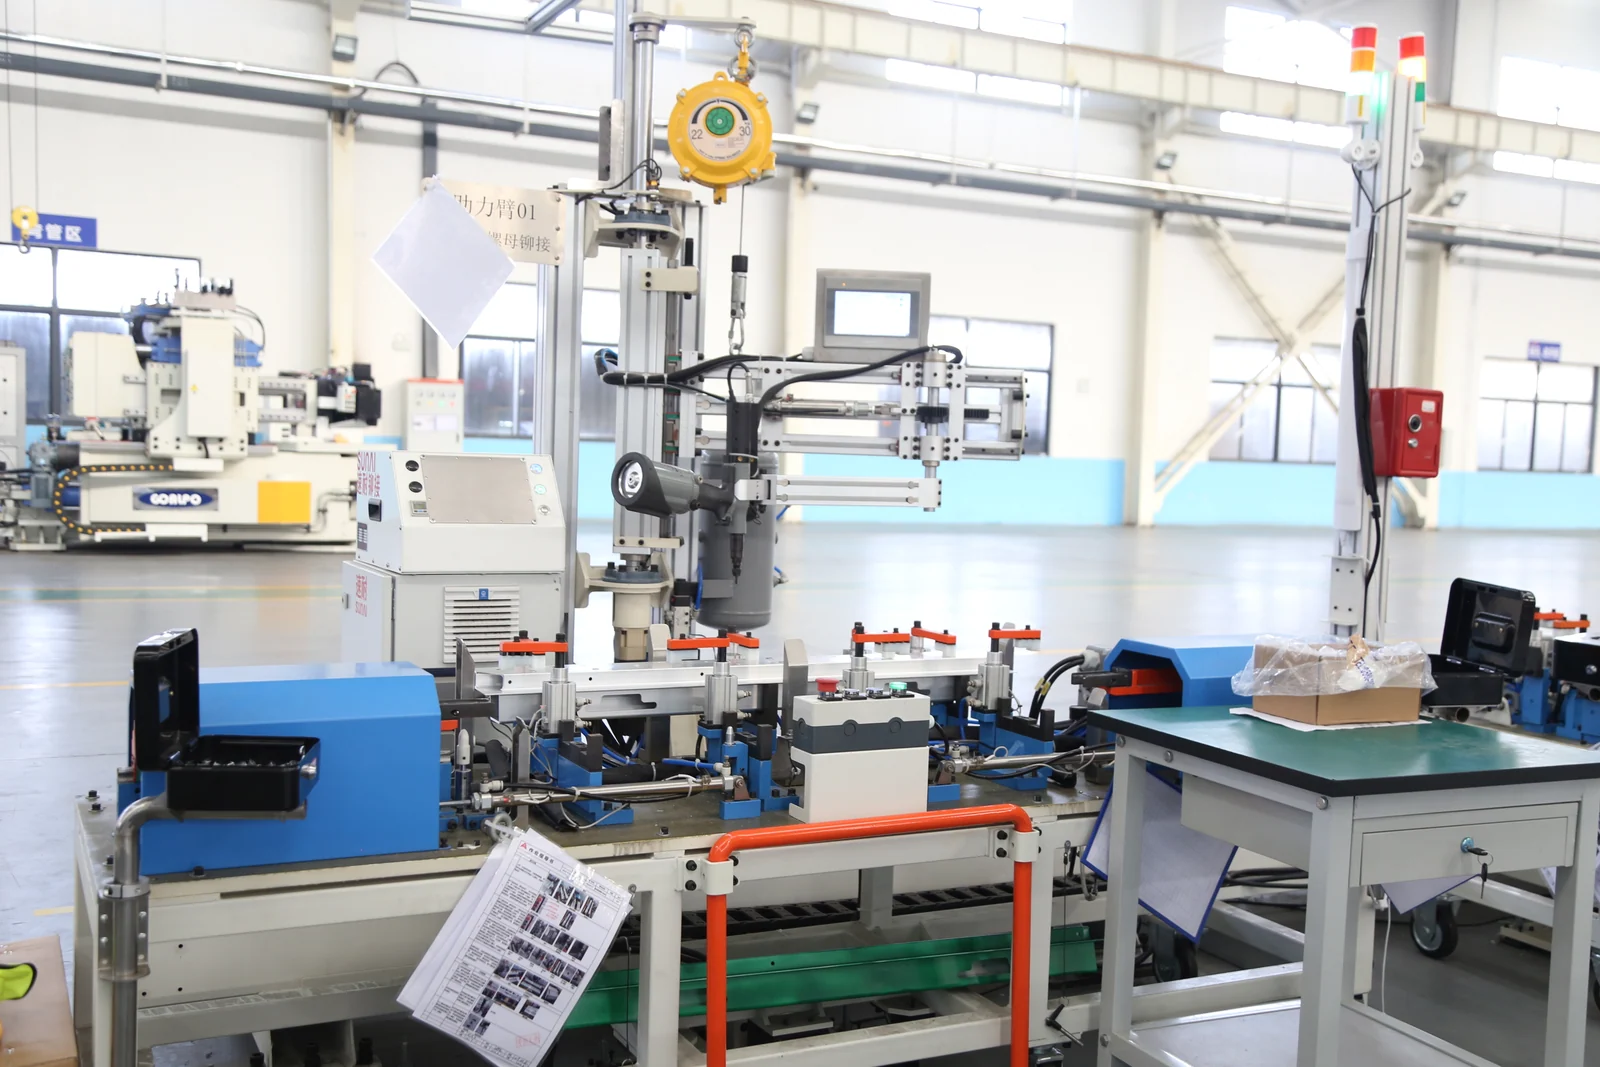
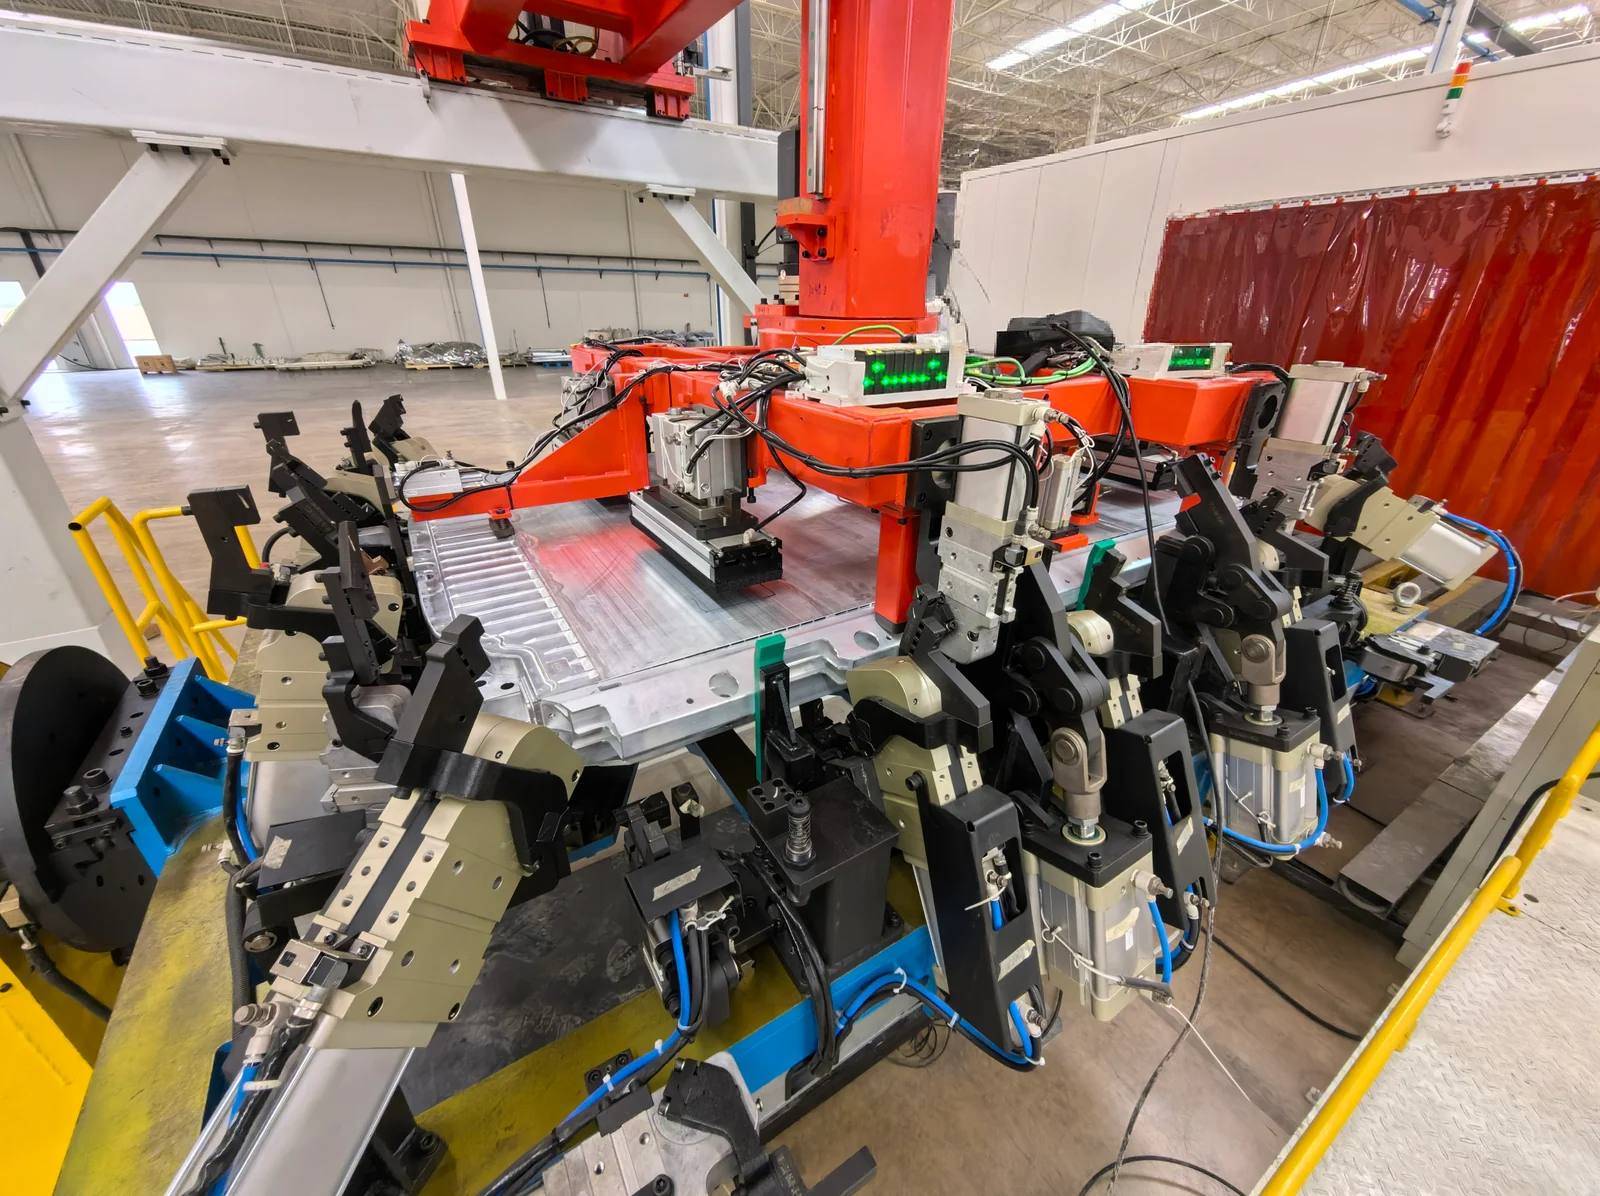
Components are joined through riveting operations. Positioning, clamping and the process mechanism are selected according to the product structure and joining requirements.

Screwdriving & Fastening

Fastener feeding, positioning, tightening and process confirmation are coordinated according to the assembly requirements.

Loading & Feeding

Loading & Feeding

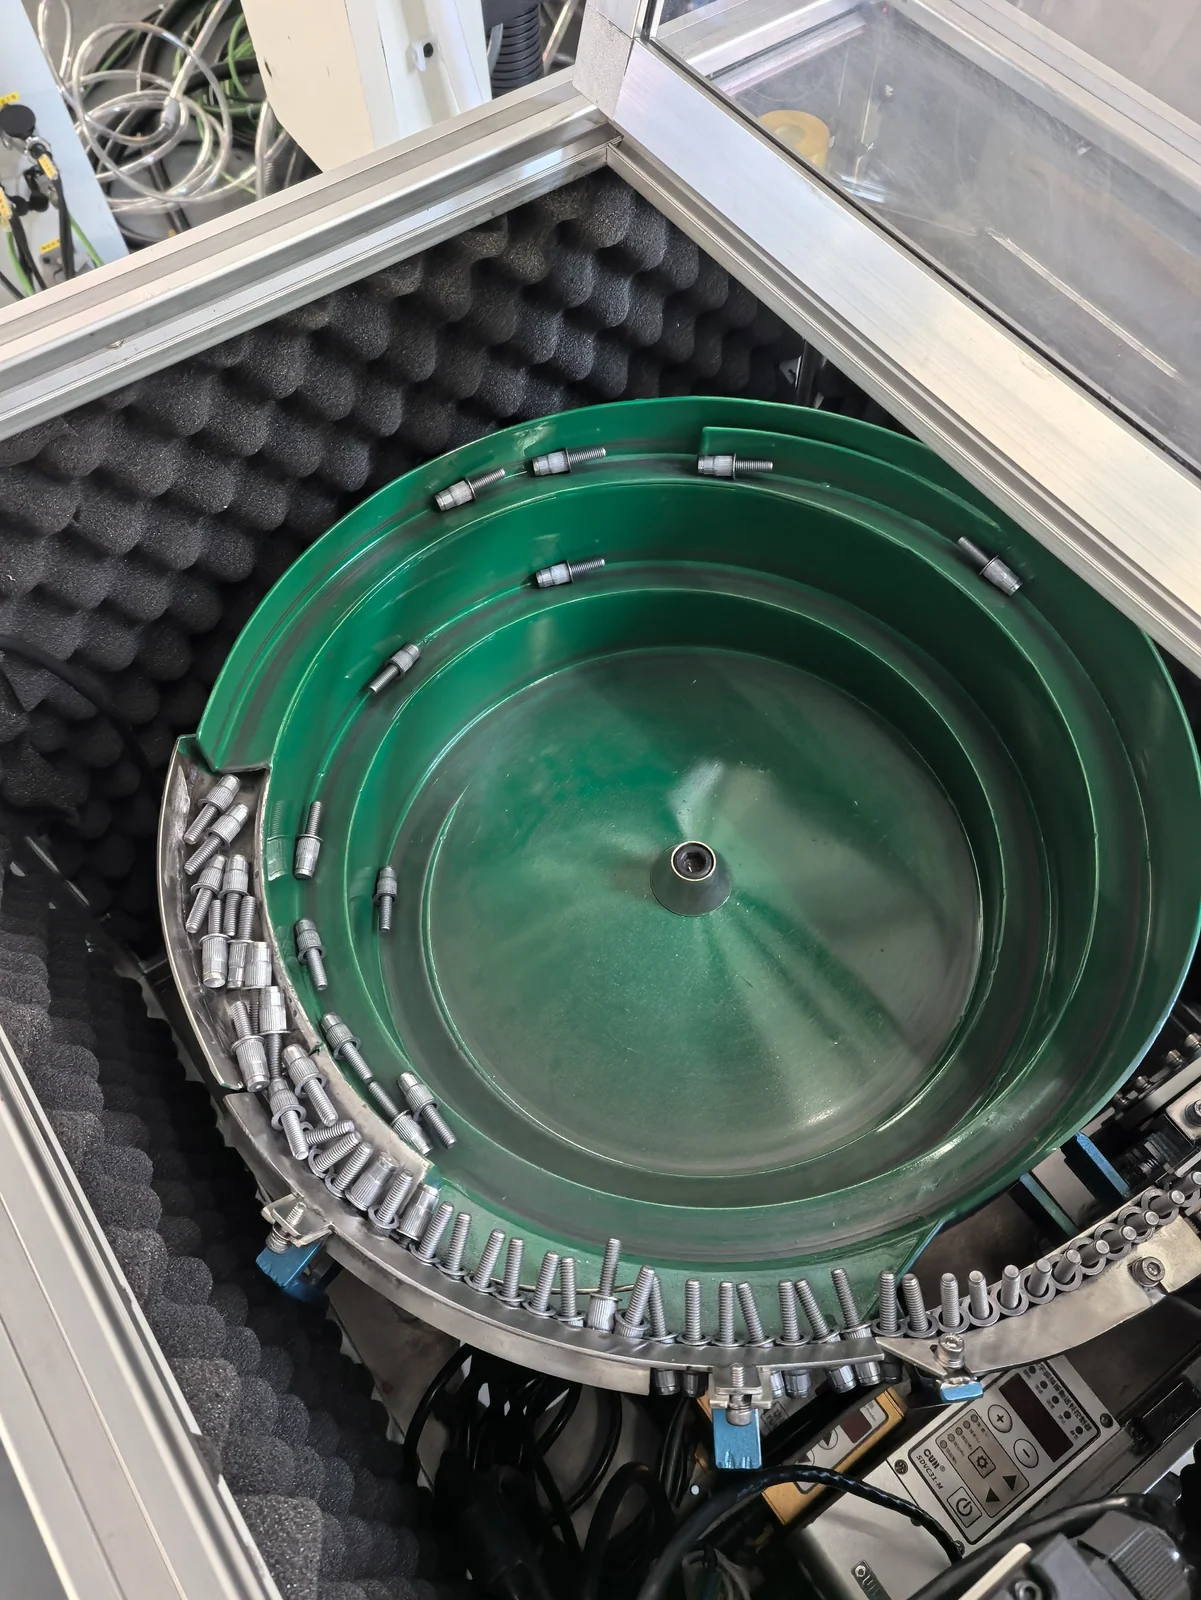
Materials are supplied to assembly stations according to their form and the production cycle. The arrangement can include manual or automated feeding, orientation and robot picking.

Positioning & Clamping

Positioning & Clamping

Positioning establishes a stable, repeatable process reference. Clamping holds the product or component in place for assembly, press-fitting, riveting or robotic operations.

An Integrated Assembly Process

  • Assembly Systems

    How the overall assembly flow is organized

  • Process Modules

    How each operation is performed at a station

  • Integrated Assembly Process

Selected Assembly & Process Projects

Automotive Aluminum Alloy Component Riveting Line

Automotive Aluminum Alloy Component Riveting Line

  • Riveting
  • Workstation layout
  • Installation & commissioning

What We Consider When Designing the Assembly System

Equipment and workstation configuration are defined by the actual product and process rather than a fixed equipment package.

View the Project Preparation Guide →

Coordinate stations, process mechanisms and controls into a reliable assembly flow.

  • Process integration
  • Station coordination
  • Process confirmation
  • Equipment interlocks

Planning an Assembly Automation Project?

Share your product, process flow, cycle time and existing layout, and we can start from the information currently available.